
 0800 118 2500
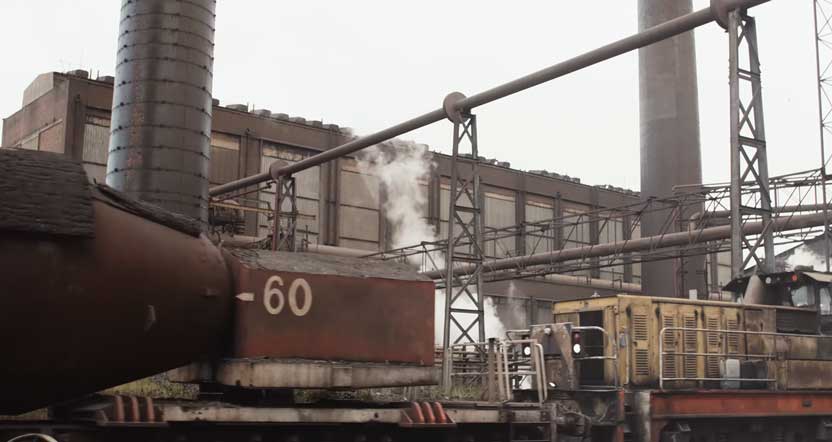
Images used are from British Steel | For the Nation. Used with the kind permission of British Steel
New Energy-efficient Pump at British Steel’s wastewater remediation plant.
A modern pump for 70℃, high pH wastewater effluent treatment system
Project Overview
Low maintenance, modern pump replaces a legacy steam-pump at British Steel
British Steel upgraded its industrial wastewater treatment system by replacing an old steam-driven unit with an automated heavy-duty industrial peristaltic pump. The pump can operate as required or on 24/7 duty, handling 70°C chemically aggressive, high pH liquor.
It is a critical component of British Steel’s drive to streamline site remediation, a project led by Jason Fisher, water and energy operations engineer. His work has resulted in a 92% reduction in stored wastewater volume over a 12-month period and ultimately sees high-purity water responsibly discharged back to the environment.
Background and Context
Responsible environmental stewardship remains central to site operations at British Steel. Managing process water and site runoff requires continuous remediation of trade effluent across the works, including drainage collected from legacy coke-making assets.
To ensure water returned to natural watercourses meets rigorous purity thresholds, British Steel operates a specialised dual-still distillation plant to break down ammonia compounds and isolate contaminants from the steel-making process.
Challenge
Managing continuous wastewater treatment across high-temperature, chemically aggressive fluid circuits puts a lot of work on pump assets and their maintenance engineers. The multi-stage treatment process takes ammoniacal wastewater from the plant through steam-stripping stills, distilling purified water from hot, concentrated mother liquor. This concentrate drops into a low-level hot well at approximately 70°C, where it must be reliably pumped back up into primary storage tanks for secondary re-distillation before final quality monitoring and eventual discharge.
The previous pumping arrangement created a few operational and reliability bottlenecks:
- Obsolete Steam-Driven Pumping: The system relied on an ageing steam-driven pump that was inefficient and labour-intensive to service
- Extreme Fluid Demands: Running at 70°C with an oily surface sheen and concentrated ammonia salts, the liquor caused accelerated wear and thermal stress on standard pump components.
- High-Head Transfer Requirements: The application required drawing fluid from the hot well via a 2 to 3 metre vertical suction lift, then discharging at 10 metres vertical head into the top of the storage vessel.
- Continuous Duty Demands: Halting fluid movement risked backing up the hot well and interrupting the stills, demanding 24/7 pumping dependability.
Under new ownership, British Steel launched an overhaul of the energy and water treatment services to stabilise operations and clear legacy wastewater backlogs. A low-maintenance, electrically driven solution was required to eliminate steam dependencies and run unattended around the clock.
Solution
Atlantic Pumps worked alongside British Steel engineer Jason Fisher to assess the process conditions and select the right pump. A heavy-duty industrial peristaltic pump was specified as the optimum method for handling hot, chemically aggressive liquids.
To match the flow rate requirements, a 3″ peristaltic pump with a variable speed drive was installed. This is hard-piped directly adjacent to the hot well for maximum energy efficiency on varying suction lift heights.
Peristaltic technology isolates the pumped fluid entirely within an elastomeric hose element, eliminating mechanical seals, valves, and rotating parts that typically succumb to chemical attack or thermal degradation.
Large Industrial Peristaltic Pump
Above: large industrial peristaltic pump with inner workings shown
The comprehensive installation package delivered robust automation and long-term operating security:
- Engineered for Thermal & Chemical Resilience: The peristaltic pump hose material used tolerates the 70°C operating temperature and aggressive mother liquor chemistry, maintaining smooth suction without vapour lock or overheating risks.
- High Vertical Lift & Discharge: Operating with positive displacement action, the pump comfortably handles the 3-metre suction lift and provides consistent pressure to transfer the concentrate 10 metres vertically into the header of the secondary distillation tank.
- Dedicated Variable Speed Drive (VSD): Equipped with an integrated inverter drive, the pump allows site operators to dial speeds up or down to balance flow rates directly with distillation throughput, laying the groundwork for full integration with hot well level sensors.
- Complete Commissioning & Practical Training: Embodying Atlantic Pumps’ commitment to doing what’s best for the customer, Atlantic Pumps field engineer Ben Whittington attended site to conduct comprehensive commissioning and deliver hands-on training to British Steel’s site team, ensuring staff were confident in operations and routine maintenance.
To discover how engineered positive displacement systems handle complex chemicals and abrasive sludges, view our full range of process improvement & optimisation services.
Results
Simple Operation – Energy Efficient – Highly Controllable 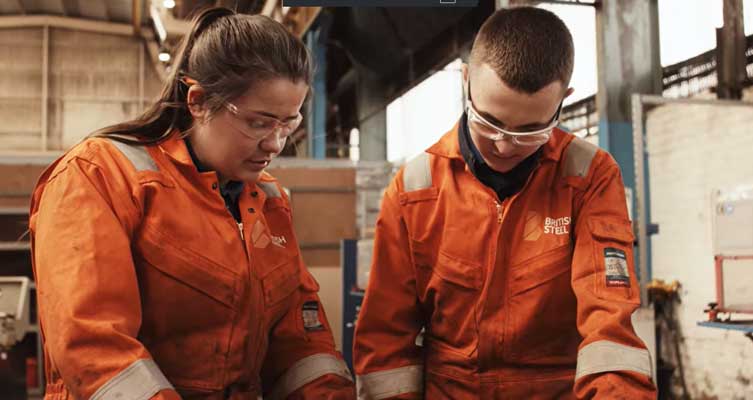
The deployment of the peristaltic pump provided an efficient, reliable transfer loop that directly enabled British Steel’s wider environmental remediation and site water management program:
- 92% Reduction in Stored Wastewater: As a reliable enabler of the multi-stage distillation circuit, the pump supported Jason Fisher’s team in shrinking total on-site wastewater storage from 100,000 litres down to just 8,000 litres.
- Unattended 24/7 Operation: The pump runs continuously on-site tick-over around the clock, maintaining stable well levels without manual intervention or temperature trips.
- Decarbonisation & Steam Elimination: Replacing the legacy steam pump reduces heat demand and downtime risk, contributing to energy efficiency and simplifying mechanical utilities.
- Minimal Maintenance & Zero Seal Failures: With only a single consumable wear hose to monitor, the site eliminated routine seal repacking, gland leaks, and unplanned downtime.
- High-Purity Environmental Compliance: Continuous transfer enables steady re-distillation through both stills, ensuring discharged process water reliably meets stringent regulatory discharge standards.
The new pump is a key enabler of our legacy wastewater management and treatment project
Jason Fisher, Energy & Water Improvement Engineer
Found this article useful?
To discover the optimal pumping solutions for your heavy industry processes, contact Euan Noakes or your account manager at Atlantic Pumps.

